
Natural and Treated Seawater Systems
Seawater intake, cooling water and firewater mains are piped in seamless 6Mo grade S31254, where chloride pitting and crevice corrosion at flange faces and gasket seats decide the material.
ASTM A312 / ASME SA-312 / UNS S31254 / W.Nr. 1.4547
Thaida Stainless Steel Manufacturing (Thailand) Co., Ltd., working from Ban Bueng, Chonburi, Thailand, manufactures SMO 254 seamless pipes (UNS S31254) to ASTM A312 for seawater, bleach plant and flue gas cleaning lines exposed to chlorides. Often called 6 Moly for its 6.0 to 6.5% molybdenum, the grade (W.Nr. 1.4547) is a high-alloy austenitic option within our stainless steel seamless pipes range. Quotations, mill certificates and export documents are issued from our Bang Phli, Samut Prakan office.
SMO 254 seamless pipeUNS S31254 / W.Nr. 1.4547
EN 10204 3.1 certificate / 3.2 on request
Order each line by NPS and stainless schedule, or by finished OD and wall from your drawing. The production envelope, end preparations, finishes and release tests for our ASTM A312 SMO 254 seamless pipe are set out below.

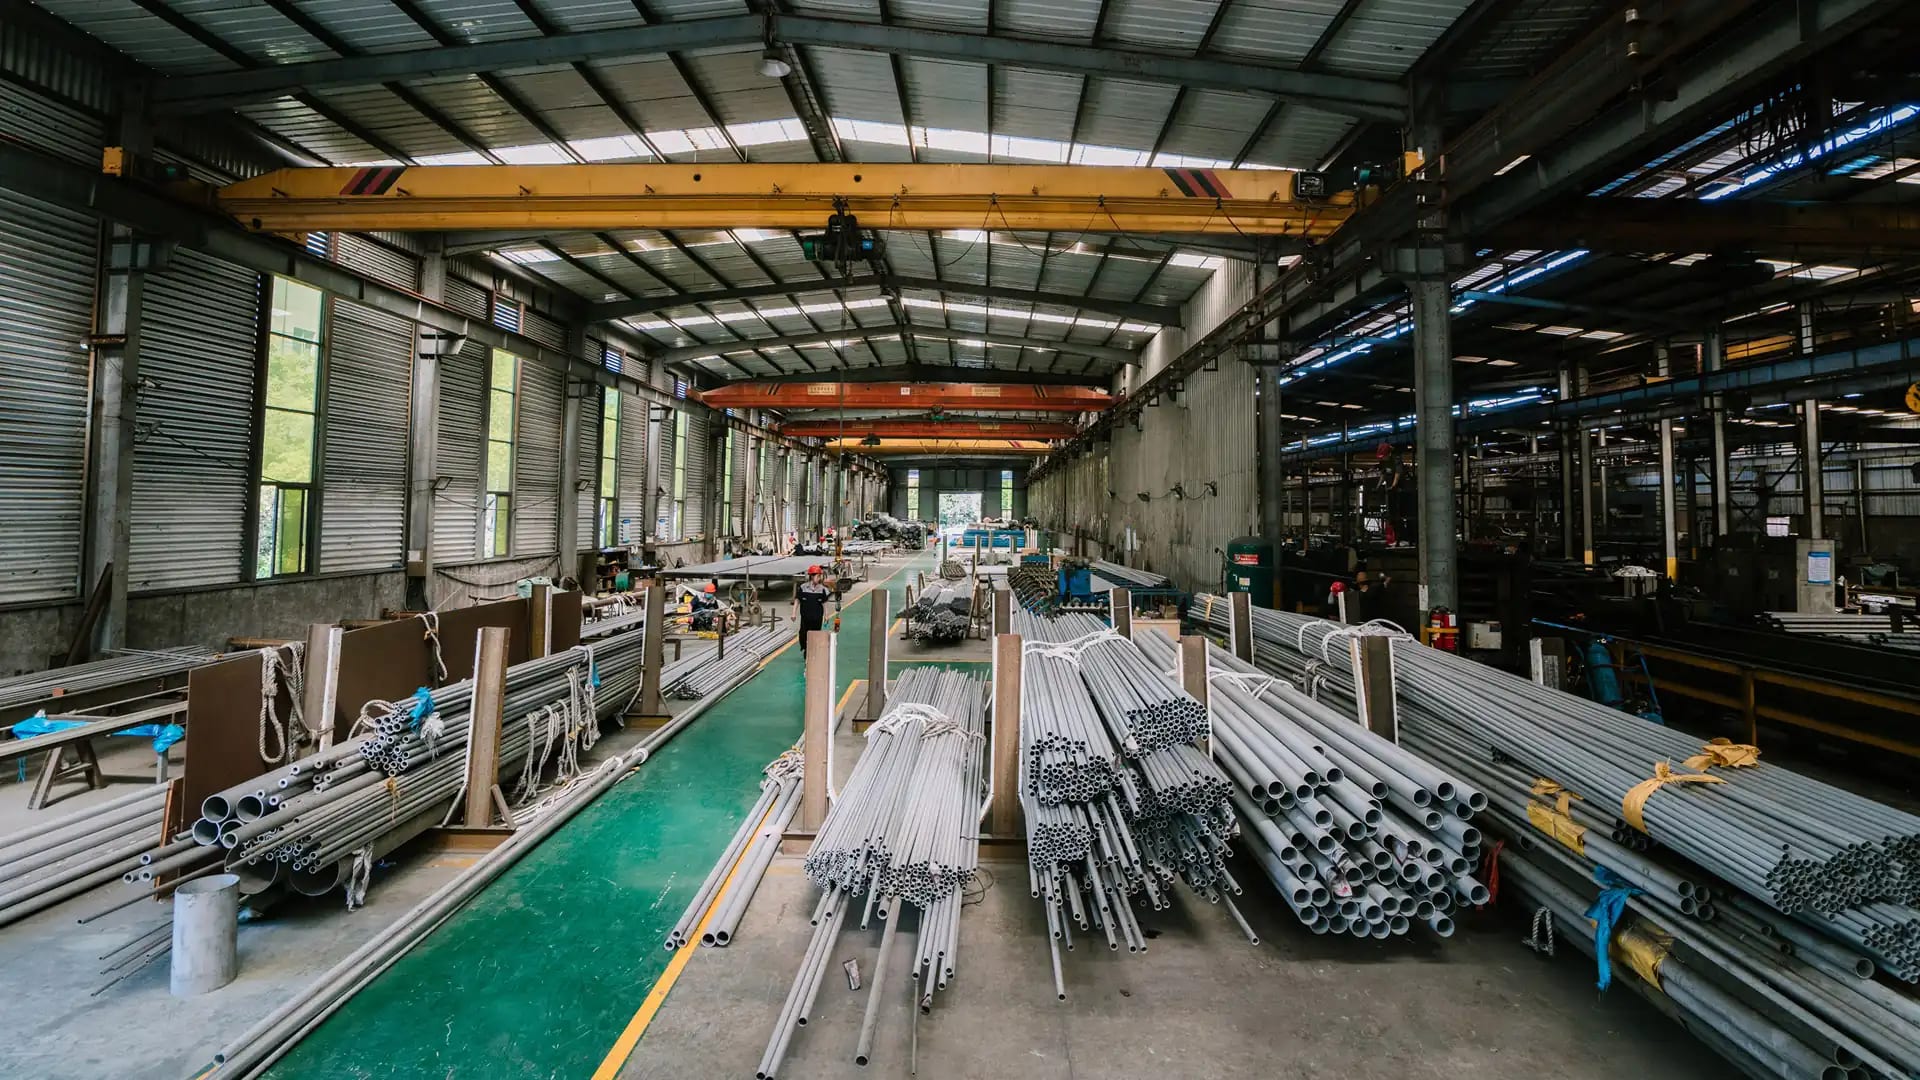
Our seamless product falls under ASTM A312 / ASME SA-312, whose scope is austenitic pipe for general corrosive and high-temperature service, and each heat is released against its requirements for UNS S31254. Pipe is hot finished or cold finished, solution annealed, and released free of scale and contaminating iron particles. ASME B36.19M fixes the standard NPS dimensions, while A312 also accepts other OD and wall combinations that meet all its remaining requirements. For heat exchanger and instrument duty sized to tube tolerances, the same alloy is made as SMO 254 seamless tubes.
For every heat, our mill issues an EN 10204 3.1 (3.2 on request) material test certificate covering the seamless WNR 1.4547 pipe made from it. One tension test covers each lot of up to 100 pipes, flattening tests are drawn from every lot, and each length passes either a hydrostatic test or a nondestructive electric test, chosen by us unless your order names one. Raw materials certificates, 100% PMI results and heat treatment charts can be added to the document set, together with surface roughness and size measurements and a test certificate from a government-approved laboratory. Third-party inspection, product analysis (S1) and intergranular corrosion testing to ASTM A262 Practice E (S7) are available on request.
Chromium at 19.5 to 20.5%, nickel at 17.5 to 18.5% and molybdenum at 6.0 to 6.5% form the base of the alloy, with 0.18 to 0.25% nitrogen and 0.50 to 1.00% copper added. Carbon is held to 0.020% and sulfur to 0.010%. Each heat cast for UNS S31254 seamless pipe is analyzed against these ASTM A312 limits, and the results appear on the mill certificate.
UNS S31254SMO 254
| Element | Limit per ASTM A312 (%) |
|---|---|
| C (Carbon) | 0.020 max |
| Mn (Manganese) | 1.00 max |
| P (Phosphorus) | 0.030 max |
| S (Sulfur) | 0.010 max |
| Si (Silicon) | 0.80 max |
| Cr (Chromium) | 19.5 to 20.5 |
| Ni (Nickel) | 17.5 to 18.5 |
| Mo (Molybdenum) | 6.0 to 6.5 |
| N (Nitrogen) | 0.18 to 0.25 |
| Cu (Copper) | 0.50 to 1.00 |
ASTM A312 gives this grade two tensile minimums, divided at a wall of 5.00 mm (0.187 in.), and a single yield minimum for every wall. Each lot is tension tested in the solution-annealed condition, and the specification sets no hardness requirement.
| Property | Value | Unit |
|---|---|---|
| Tensile Strength, min, wall 5.00 mm and under | 675 (98) | MPa (ksi) |
| Tensile Strength, min, wall over 5.00 mm | 655 (95) | MPa (ksi) |
| Yield Strength, min | 310 (45) | MPa (ksi) |
| Elongation in 2 in. or 50 mm, min, longitudinal | 35 | % |
| Elongation in 2 in. or 50 mm, min, transverse | 25 | % |
Drawings and data sheets refer to SMO 254 by several designations; the American, European and Chinese ones are shown below.
These designations serve as cross-references only. Our certificate states ASTM A312 UNS S31254, which is the grade supplied when a line list calls for seamless 1.4547 stainless steel pipe.
Our seamless SMO 254 stainless steel pipe spans 6 mm to 1016 mm in OD and 1 mm to 65 mm in wall, delivered in single lengths up to 18 m or cut to order. Standard NPS sizes take their dimensions from ASME B36.19M, and non-standard OD and wall combinations from drawings are produced within the same limits.
For seawater and cooling water headers, the rows below give Sch 5S, 10S and 40S nominal walls in mm from NPS 2-1/2 to NPS 20, taken from ASTM A312 Table X1.1:
| NPS | OD (mm) | Sch 5S | Sch 10S | Sch 40S |
|---|---|---|---|---|
| 2-1/2 | 73.0 | 2.11 | 3.05 | 5.16 |
| 6 | 168.3 | 2.77 | 3.40 | 7.11 |
| 10 | 273.1 | 3.40 | 4.19 | 9.27 |
| 14 | 355.6 | 3.96 | 4.78 | 9.53 |
| 20 | 508 | 4.78 | 5.54 | 9.53 |
Swipe sideways to see the full table.
Sch 80S and walls up to 65 mm are produced for pressure headers outside these rows.
Every size may fall 12.5% below nominal wall. How far it may exceed nominal is set by NPS and by t/D, the ratio of wall to OD:
| NPS | t/D | Over Nominal (%) | Under Nominal (%) |
|---|---|---|---|
| 1/8 to 2-1/2 | All | 20.0 | 12.5 |
| 3 to 18 | 5% or less | 22.5 | 12.5 |
| 3 to 18 | Over 5% | 15.0 | 12.5 |
| 20 and larger | 5% or less | 22.5 | 12.5 |
| 20 and larger | Over 5% | 15.0 | 12.5 |
Swipe sideways to see the full table.
By nominal diameter (DN), A312 pipe is held to these OD limits:
| DN | OD Tolerance (mm) |
|---|---|
| 6 to 40 | +0.4 / -0.8 |
| Over 40 to 100 | +0.8 / -0.8 |
| Over 100 to 200 | +1.6 / -0.8 |
| Over 200 to 450 | +2.4 / -0.8 |
| Over 450 to 650 | +3.2 / -0.8 |
| Over 650 to 850 | +4.0 / -0.8 |
| Over 850 to 1200 | +4.8 / -0.8 |
A definite cut length is held to the ordered figure on the minus side, with up to 6 mm (1/4 in.) allowed over.
Spool shops join SS SMO 254 seamless pipe mainly by butt welding, with flanges at pumps, valves and equipment nozzles. Sch 5S and 10S walls are too thin for ASME B1.20.1 pipe threads, so screwed joints are reserved for Sch 40S and 80S. We cut lengths to your spool list and bevel the ends to the angle and root face of your weld procedure, while plain ends are left square for socket fittings or site preparation. Every length is marked SML with its heat number, so each spool piece can be traced back to its certificate after cutting.
904L seamless pipes and SMO 254 are both high-alloy austenitic grades that ASTM A312 lists by UNS number, but their chemistry points in different directions. UNS N08904 carries 23.0 to 28.0% nickel, 4.0 to 5.0% molybdenum and 1.00 to 2.00% copper, the copper aimed at sulfuric acid. UNS S31254 carries 6.0 to 6.5% molybdenum and 0.18 to 0.25% nitrogen, the combination behind its chloride pitting and crevice resistance, and its 310 MPa yield minimum sits well above the 215 MPa set for N08904.
For milder process water and general chemical duty, 316L seamless pipes are the lower-alloy molybdenum-bearing option. SMO 254 comes in where seawater, brine or other chloride-rich media set the material.
Plants specify SMO 254 stainless steel seamless pipe where chloride stress corrosion cracking, pitting and crevice corrosion would shorten the life of a piping system.
Seawater intake, cooling water and firewater mains are piped in seamless 6Mo grade S31254, where chloride pitting and crevice corrosion at flange faces and gasket seats decide the material.
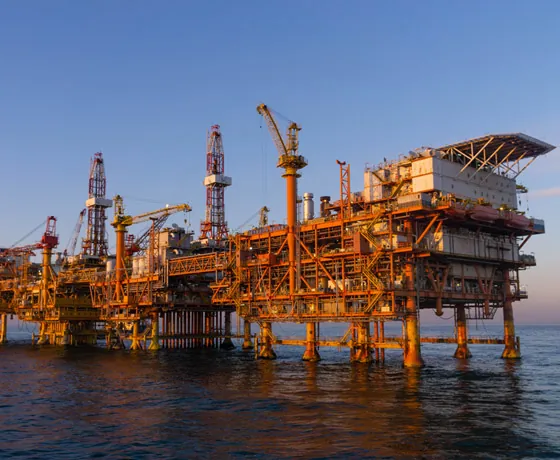
Offshore and onshore production facilities run UNS S31254 seamless pipe in seawater injection, produced water and utility lines, ordered by NPS and schedule to match the project piping class.

Scrubber recirculation, quench and absorber feed lines in flue gas cleaning units carry acidic, chloride-laden liquor, and their spools are butt welded from seamless S31254 stainless steel pipe in Sch 10S or 40S.

Chlorine dioxide bleaching stages, with their washer and filtrate lines, handle chloride-bearing liquors, so pulp and paper mills pipe them in SMO 254 with beveled ends ready for site welding.

Fertilizer plants use seamless 6Mo pipe for cooling water and chloride-contaminated process streams, from small-bore sampling lines to large-diameter headers ordered by OD and wall.
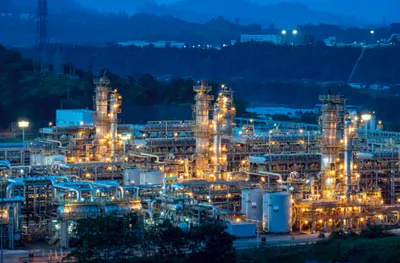
Refineries and petrochemical complexes route seawater-cooled exchanger connections and chloride-bearing process streams through ASTM A312 S31254 stainless steel seamless pipe, tested length by length before release.
Packing
Export wooden cases, or bundles sleeved in woven bags and sized for container loading.
Marking
ASTM A312, UNS S31254, SML, heat number and size stenciled on each length.
End protection
Plastic end caps on every length, with bevels shielded from knocks in transit.
Documents
Packing list plus the EN 10204 3.1 (3.2 on request) certificate for each heat shipped.
Shipment basis
FOB, CFR or CIF.
Timing
Each line item's dispatch date is stated on the quotation.
Indicative market levels put SMO 254 stainless steel seamless pipe to ASTM A312 at around USD 11 to 20 per kg. Molybdenum at 6.0 to 6.5% and nickel at 17.5 to 18.5% set the base cost, while heavy walls, large diameters, small lots and added testing move an order toward the top of the band. We confirm a firm figure once your sizes and test requirements are in hand.
Indicative only. Send your sizes and specification to Thaida for a firm quotation.
Each length we sell is hot or cold finished and solution annealed at our factory, 154 Moo.1 Map Phai, Ban Bueng, Chonburi 20170, Thailand. Technical queries and contract paperwork are handled by our Bang Phli office, located at 89/18 Moo.15 Enterprize Park, Bangna-Trad Road, Bang Kaeo, Bang Phli, Samut Prakan 10540, Thailand. Export orders travel to Singapore, Malaysia, Vietnam, Indonesia, the Philippines and India, and domestic orders to sites throughout Thailand.
Yes, if your pressure design allows. ASTM A312 Table X1.1 gives Sch 10S walls of 3.05 mm at NPS 2-1/2 up to 5.54 mm at NPS 20. Through NPS 18 those walls are 5.00 mm or less and need 675 MPa (98 ksi) tensile, while the 5.54 mm wall at NPS 20 takes the 655 MPa (95 ksi) minimum.
Yes. ASTM A312 permits 0.18 to 0.25% nitrogen in UNS S31254, so a heat at 0.23% complies. If your project specification sets a narrower nitrogen window, write it on the inquiry and we confirm before production that the heat meets both limits.
AWS ERNiCrMo-3 or ERNiCrMo-10 filler is recommended for seamless WNR 1.4547 pipe (UNS S31254). Both are nickel-chromium-molybdenum classifications, so qualify your weld procedure with the chosen wire before production welding of the spools starts.
By 100% PMI. Positive material identification is available on every length and its records join the certificate pack, so a heat with 6.0 to 6.5% molybdenum is confirmed before the pipe leaves the mill. When your order needs a full laboratory check on finished pipe, add product analysis under ASTM A312 supplementary requirement S1.
It can help. After significant cold working, solution annealing at 1150 to 1200 °C followed by a water quench may be beneficial for UNS S31254. Pipe from our mill already arrives in that condition, annealed at 1150 °C (2100 °F) minimum as ASTM A312 requires, so the question arises only for pieces formed during fabrication.
Either one. Both finishes are available on seamless S31254 stainless steel pipe. Pickling and passivation remove scale chemically after annealing, while ASTM A312 makes pickling unnecessary for bright annealed pipe. Polished, mirror and brushed surfaces are further options, and the finish can differ from one line item to the next on the same order.
Because UNS S31254 contains more than 3% molybdenum. For such grades, ASTM A312 supplementary requirement S7 (ASTM A262 Practice E) leaves the applicability of the test and the sample preparation to agreement with the manufacturer. Name S7 on the inquiry and we settle both points with you before production.
Request a Quote for SMO 254 Seamless Pipes
or email sales@thaida.co.th