
Offshore Firewater and Seawater Injection
Offshore topsides run the alloy in seawater and firewater systems, and seawater injection plants use it for headers and distribution lines, each sized by NPS and schedule from the project piping class.
ASTM A312 / ASME SA-312 / UNS N08926 / W.Nr. 1.4529
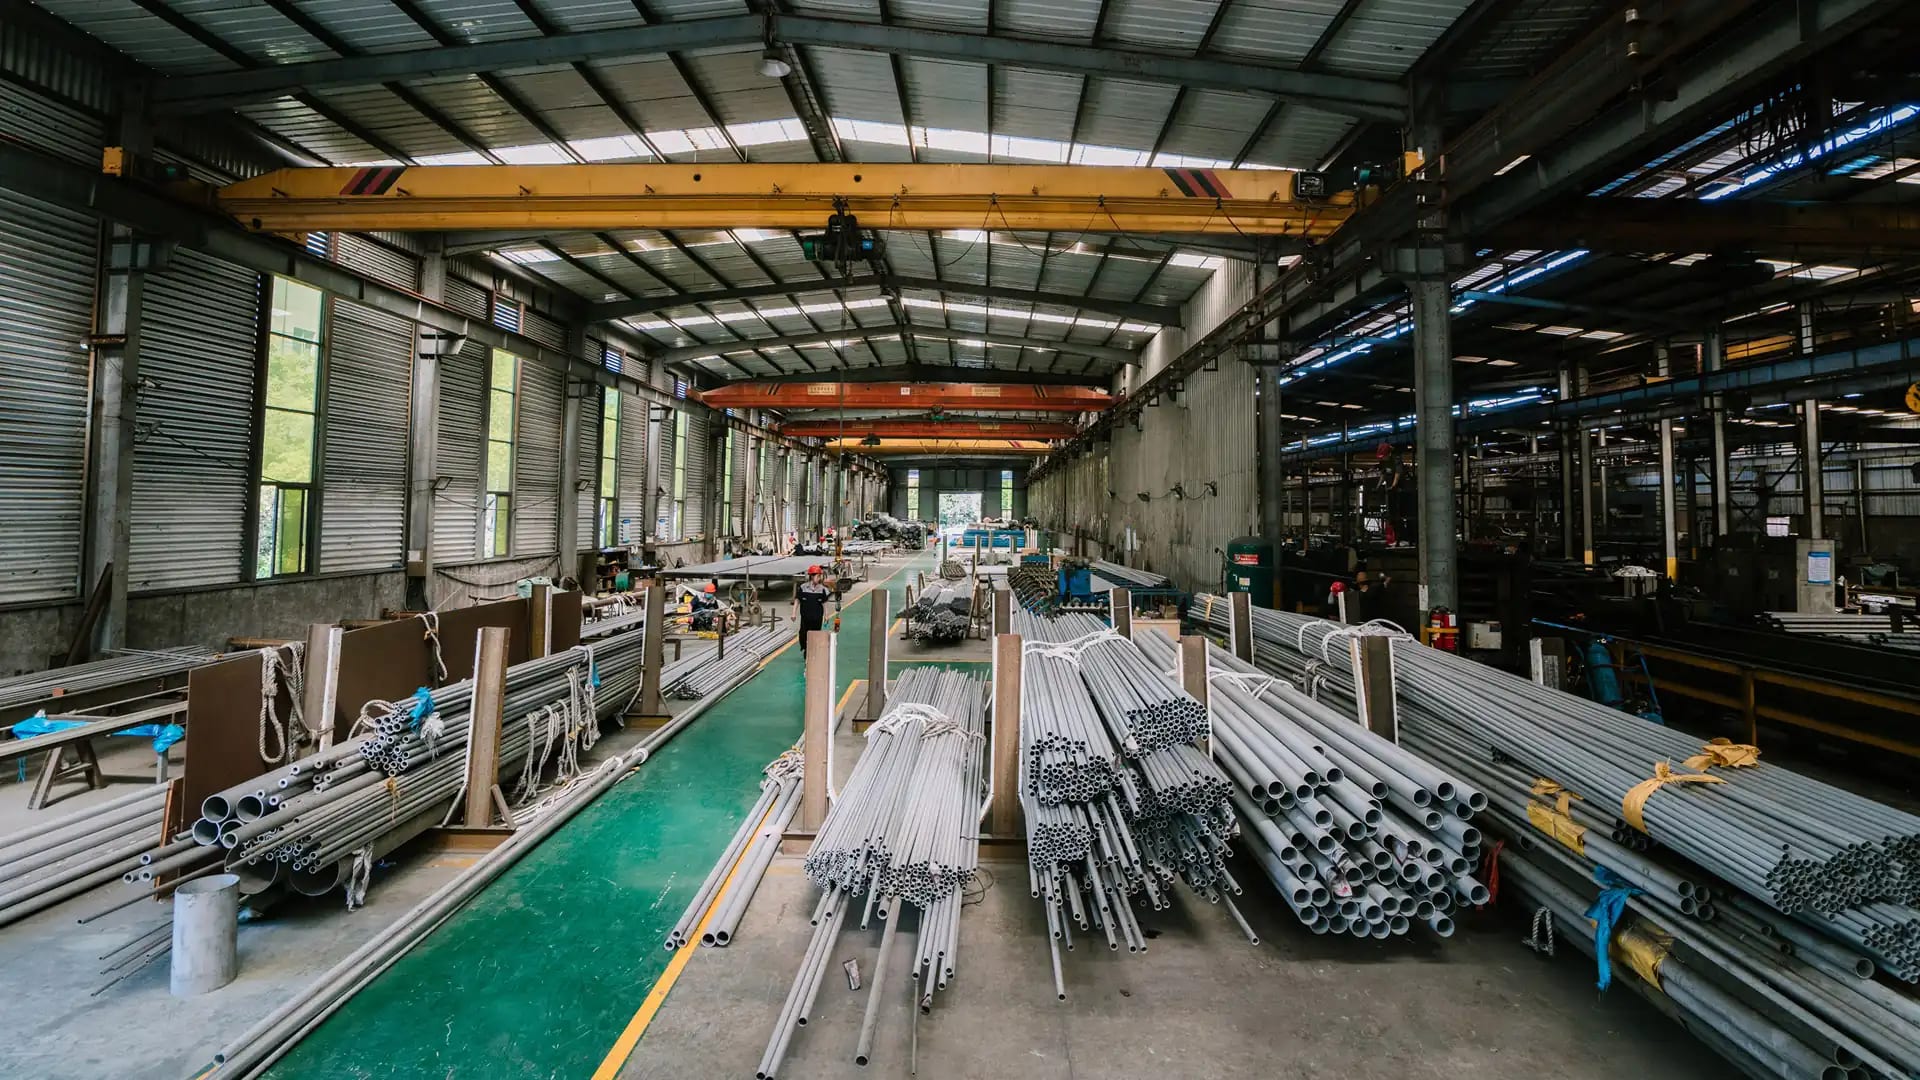
Alloy 926 seamless pipes from Thaida Stainless Steel Manufacturing (Thailand) Co., Ltd. carry seawater, firewater, brine and chloride-bearing acid streams in offshore, desalination, bleach plant and flue gas cleaning service. Every length is produced at our Ban Bueng, Chonburi mill to ASTM A312 / ASME SA-312 in UNS N08926 (W.Nr. 1.4529), a high-molybdenum austenitic alloy with nitrogen and copper that belongs to our Incoloy seamless pipes range. Our Bang Phli, Samut Prakan office handles every quotation and certificate.
Alloy 926 seamless pipeUNS N08926 / W.Nr. 1.4529
EN 10204 3.1 certificate / 3.2 on request
Lines are ordered by NPS and schedule or by outside diameter and wall, and each one is quoted inside the envelope shown here. The heat treatment ASTM A312 requires for UNS N08926 and the release tests applied to every lot are listed alongside.

Seamless pipe in this alloy falls under ASTM A312, which lists the grade by its UNS number alone, so N08926 is the designation marked on each ASTM A312 UNS N08926 seamless pipe and printed on its certificate. For Boiler and Pressure Vessel Code applications, the related specification is ASME SA-312, and code lines are written as ASME SA-312 UNS N08926 seamless pipe. Within our Incoloy range the alloy is also requested as seamless Incoloy 926 pipe, and those lines are made to the same UNS N08926 requirements. For exchanger and condenser bundles sized to tube tolerances, the alloy is produced as Alloy 926 seamless tubes.
A lot of up to 100 pipes is tension tested once, and a lot of more than 100 pipes twice. Flattening tests are made on 5% of each lot, and each length is proved by a hydrostatic test or by a nondestructive electric test (eddy current or ultrasonic), at our choice unless the purchase order names the method. An EN 10204 3.1 (3.2 on request) material test certificate travels with every shipment. Third-party inspection and the intergranular corrosion test of supplementary requirement S7 are available on request.
Molybdenum is held at 6.0 to 7.0% and nitrogen at 0.15 to 0.25%, with nickel at 24.0 to 26.0%, chromium at 19.0 to 21.0% and copper at 0.50 to 1.50%, and iron makes up the balance. Carbon is capped at 0.020% and sulfur at 0.010%. Every heat cast for seamless WNR 1.4529 pipe is analyzed against these limits.
UNS N08926926
| Element | Limit per ASTM A312 / ASME SA-312 (%) |
|---|---|
| C (Carbon) | 0.020 max |
| Mn (Manganese) | 2.00 max |
| P (Phosphorus) | 0.030 max |
| S (Sulfur) | 0.010 max |
| Si (Silicon) | 0.50 max |
| Cr (Chromium) | 19.0 to 21.0 |
| Ni (Nickel) | 24.0 to 26.0 |
| Mo (Molybdenum) | 6.0 to 7.0 |
| N (Nitrogen) | 0.15 to 0.25 |
| Cu (Copper) | 0.50 to 1.50 |
ASTM A312 gives UNS N08926 a single tensile and yield minimum for every wall, with separate elongation minimums for longitudinal and transverse test pieces. The specification sets no hardness requirement for the pipe.
| Property | Minimum |
|---|---|
| Tensile Strength | 650 MPa (94 ksi) |
| Yield Strength | 295 MPa (43 ksi) |
| Elongation in 2 in. or 50 mm, longitudinal | 35% |
| Elongation in 2 in. or 50 mm, transverse | 25% |
These minimums apply in the solution-treated condition. ASTM A312 calls for solution treatment at 2010 to 2100 °F (1100 to 1150 °C) followed by quenching in water or rapid cooling by other means, or, for seamless pipe, a direct quench after hot forming while the metal is still at or above the minimum solution temperature. The lot tension result for each seamless alloy N08926 pipe is reported on the certificate against these figures.
Project specifications written in Europe may give the material as 1.4529 or by its EN steel name rather than its UNS number. Because ASTM A312 identifies the grade only as UNS N08926, the rows below are cross-references for matching such a callout and claim no conformity with a European product standard.
When a requisition quotes 1.4529 or X1NiCrMoCuN25-20-7, we enter the line as UNS N08926 and certify the heat to that number.
Seamless 1.4529 alloy pipe is made from 6 mm to 457 mm OD with walls from 1 mm to 65 mm, in lengths up to 18 m. Standard sizes take the ASME B36.19 dimensions listed in ASTM A312 Table X1.1, and A312 also accepts other OD and wall pairings that meet all its remaining requirements.
In the A312 permitted variations below, the wall may run 12.5% under nominal, while the allowance over nominal depends on NPS and on t/D, the ratio of wall thickness to outside diameter:
| NPS | t/D | Over Nominal Wall | Under Nominal Wall |
|---|---|---|---|
| 1/8 to 2 1/2 | All | 20.0% | 12.5% |
| 3 to 18 | Up to 5% | 22.5% | 12.5% |
| 3 to 18 | Over 5% | 15.0% | 12.5% |
Swipe sideways to see the full table.
Lengths ordered to a definite cut are never shorter than the ordered figure and may exceed it by up to 1/4 in. (6 mm). Ends leave the mill square cut, or beveled to the angle and root face written on the order, so lengths go straight into spool fabrication.
Fabricators join seamless Incoloy 926 pipe by GTAW, GMAW or SMAW, normally as butt welds in shop spools with flanged connections at pumps, valves and vessel nozzles. Each length arrives solution treated as ASTM A312 requires, ready to be cut to the spool isometrics and prepared for welding. Each length carries its heat number, which the fabricator transfers to every cut piece so that spools trace back to the certificate.
ASTM A312 lists the grade behind our stainless steel 904L seamless pipes as UNS N08904, with 4.0 to 5.0% molybdenum and 0.10% maximum nitrogen, against 6.0 to 7.0% and 0.15 to 0.25% for N08926. The same standard holds seamless SMO 254 pipe (UNS S31254) at 6.0 to 6.5% molybdenum and 17.5 to 18.5% nickel, where N08926 carries 24.0 to 26.0% nickel.
Our Incoloy 028 seamless pipes, also listed in A312, are built around 26.0 to 28.0% chromium and 30.0 to 34.0% nickel, with 3.0 to 4.0% molybdenum and no nitrogen requirement.
Seamless Alloy 926 pipe is chosen where pitting, crevice corrosion and stress corrosion cracking in chloride media set the material, and its copper content helps in sulfuric and phosphoric acid streams.
Offshore topsides run the alloy in seawater and firewater systems, and seawater injection plants use it for headers and distribution lines, each sized by NPS and schedule from the project piping class.

Supply and return lines that carry seawater to and from cooling-water exchangers are piped in UNS N08926, with butt-welded spools built from cut lengths with beveled ends.

Desulfurization units move acidic, chloride-rich slurries through slurry piping and spray nozzle headers made from the alloy, with the wall selected from the schedule list to suit the pump pressure.

Chlorine dioxide bleaching stages in pulp mills handle chloride-bearing liquors, and their process lines are installed in this alloy with a lot certificate traceable to every heat.
Pharmaceutical plants route mixed acids and organic chlorides through the alloy, while chlor-alkali, bleach production and hydrochloric acid handling units use it for process piping between reactors, tanks and pumps.

Multi-stage flash and reverse-osmosis desalination plants install the alloy in high-pressure piping and in the lines serving brine heaters, where brine and seawater flow without interruption.
Packing
Lengths are strapped in bundles on timber skids, while smaller sizes and beveled lengths travel in export wooden cases.
Marking
Every UNS N08926 seamless pipe carries the manufacturer's mark, NPS or OD with schedule or average wall, heat number, SML and NH, ET or UT as applicable.
End protection
A plastic cap on each end, with bevels guarded against knocks in transit.
Documents
A packing list per bundle or case, plus the EN 10204 3.1 (3.2 on request) material test certificate for each heat.
Terms
FOB, CFR or CIF from the port stated in our quotation.
Timing
Each line's dispatch date appears on the order acknowledgement.
Indicative pricing for ASME SA-312 UNS N08926 seamless pipe runs from USD 20 to 45 per kg. Movements in the nickel and molybdenum markets decide most of where an offer lands within that band. Size, wall and length fix how much processing each kilogram needs, and short cut lengths, small lots or extra inspection push a figure upward. Send the NPS and schedule or OD and wall, length and quantity for each line to receive a firm price.
Indicative only. Send your sizes and specification to Thaida for a firm quotation.
Our factory at 154 Moo.1 Map Phai, Ban Bueng, Chonburi 20170, Thailand, makes and tests every length of Alloy 926 seamless pipe. Quotations, certificates and export documents are issued from our office at 89/18 Moo.15 Enterprize Park, Bangna-Trad Road, Bang Kaeo, Bang Phli, Samut Prakan 10540, Thailand. We supply projects in Thailand, Singapore, Malaysia, Vietnam, Indonesia, the Philippines and India.
ASTM A312 holds molybdenum at 6.0 to 7.0% and nitrogen at 0.15 to 0.25%, and the certificate reports the heat analysis against those ranges. A product analysis of finished pipe is made only at the purchaser's request, so add supplementary requirement S1 to the order if your quality plan needs the alloy confirmed on the pipe itself.
They are higher. ASTM A312 sets 650 MPa (94 ksi) tensile and 295 MPa (43 ksi) yield minimums for UNS N08926, against 490 MPa (71 ksi) and 215 MPa (31 ksi) for UNS N08904. Base the wall calculation on the grade actually ordered, because the certificate is read against that grade's row.
Give NPS and schedule for standard sizes, or OD and wall for sizes taken from a drawing, then the length, quantity and certificate level. Every line is checked against our range of 6 to 457 mm OD, 1 to 65 mm wall and lengths up to 18 m before the quotation is issued.
Each length receives a hydrostatic test or a nondestructive electric test (eddy current or ultrasonic), at our choice unless your purchase order fixes the method. From NPS 10 upward, with our agreement, you may waive the hydrostatic test when you will test the completed system; those lengths are marked NH, and the certificate states which test each length received.
Only when your project specification calls for it. The intergranular corrosion test is ASTM A312 supplementary requirement S7 and runs only when ordered. Because UNS N08926 contains more than 3% molybdenum, A312 makes the applicability of the test and the preparation of the sample a matter of agreement between you and us, so settle both before production.
Matching filler is the normal pairing, although some welding procedures specify an over-alloyed filler metal instead. Qualify the procedure with the filler you select before production welding starts, and name it on the spool drawings so site welders use the same wire.
The heat analysis against the A312 limits for UNS N08926, the lot tension test results, and whether each length was hydrostatically tested or, where an electric test was used, which standard practice and reference discontinuities applied. Issued to EN 10204 3.1 (3.2 on request), it repeats the heat number stenciled on each length.
Request a Quote for Alloy 926 Seamless Pipes
or email sales@thaida.co.th